Valve Commissioning Checks Before Handing an Actuated Valve to Operations
An actuated valve commissioning checklist is a structured field-verification framework for commissioning engineers, instrument technicians, and operations teams. It helps confirm that an installed actuated valve is correctly identified, connected, stroked, signaled, interlocked, and documented before routine operation. Shanghai Juliang Valve Group’s public product page presents industrial valve categories including pneumatic, electric, solenoid, control, angle-seat, manual, corrosion-resistant, and customized valves, making this a relevant general topic for B2B valve projects.
What should a commissioning team verify before operating an actuated valve?
A commissioning team should verify tag identity, installation orientation, piping cleanliness, utility supply, wiring, command and feedback signals, stroke direction, travel limits, local and remote modes, interlocks, documented exceptions, and approved site procedures before handing an actuated valve to operations.
This is not the same as a factory acceptance test. A FAT may review documents, assembly, and functional behavior before shipment. Commissioning checks confirm whether the valve, actuator, accessories, field wiring, utilities, control logic, and operating context work together after installation. For an international project team, the checklist should be treated as a handover control point, not as a substitute for the plant commissioning plan, safety procedures, or regulatory approval.
How is commissioning different from a factory acceptance test?
Commissioning verifies the installed system in its actual field environment, while a factory acceptance test verifies agreed items before shipment or release from the supplier’s facility.
A factory test cannot fully prove that the site cable terminations, instrument air header, junction boxes, control-system scaling, process interlocks, pipe supports, or final installation orientation are correct. It also cannot confirm whether the plant’s approved operating procedure has been followed. Think of it like buying a tested appliance: the factory can test the appliance, but someone still has to confirm the plug, voltage, location, ventilation, and user controls after installation. Actuated valves are more complex because wrong travel direction, unclear feedback, or bypassed interlocks can affect process operation.
Why does a structured handover checklist matter?
A structured checklist reduces the chance that hidden installation or integration issues are transferred to operations as normal equipment.
If these issues are not addressed, operations may receive a valve that appears ready but has mismatched open and closed feedback, reversed actuator movement, incomplete travel, blocked utilities, undocumented overrides, or unresolved construction damage. These problems can delay startup, confuse control-room responses, or lead to unnecessary troubleshooting. For commissioning engineers and instrument technicians, the value of the checklist is traceability. It creates a clear record of what was verified, who accepted exceptions, and which items remain under controlled follow-up.
What should be checked first at the valve location?
Start by confirming that the installed valve matches the project tag, line location, flow direction, and orientation shown in approved drawings and installation documents.
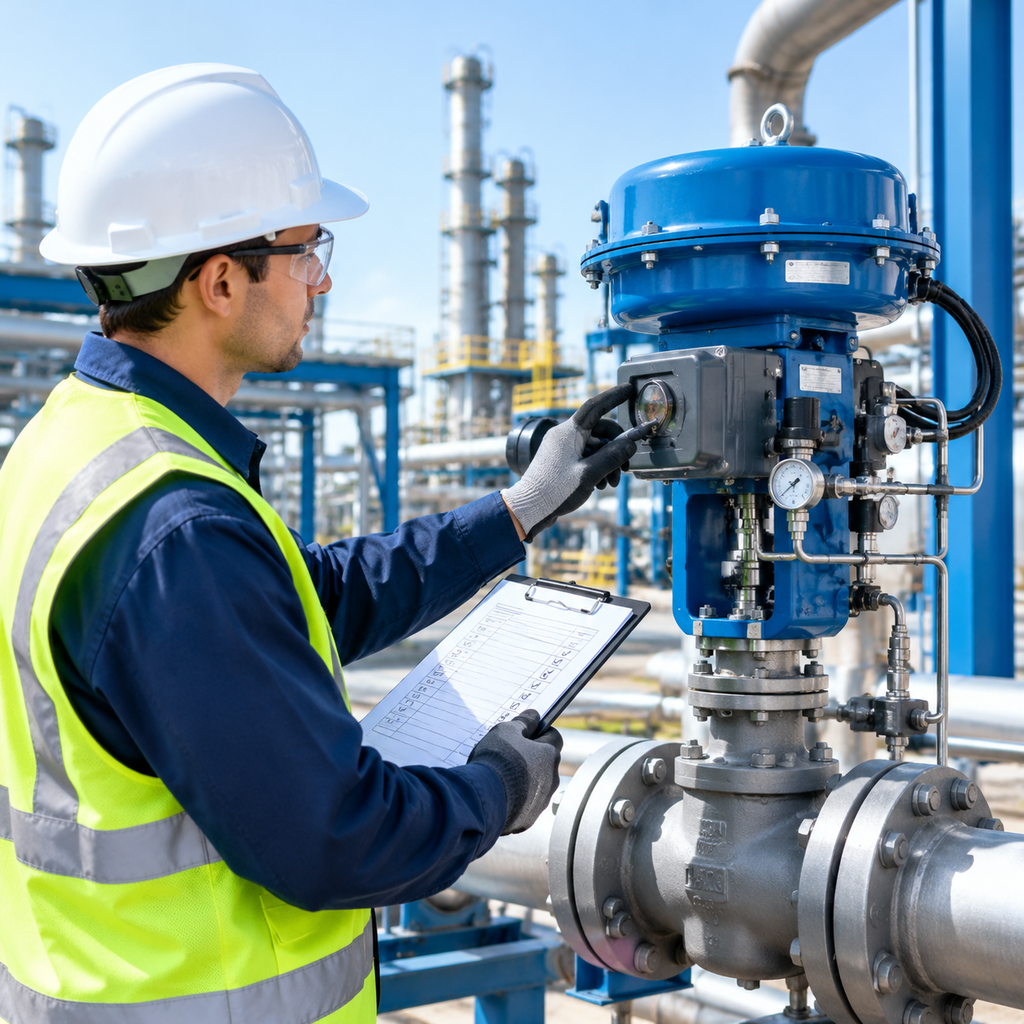
The nameplate, tag plate, actuator label, accessory tags, and cable or tubing identifiers should be readable and consistent with the handover package. The valve body orientation should be checked against the intended flow direction where the design requires it. Actuator position, handwheel access, solenoid location, limit switch access, and clearance for maintenance should also be reviewed. If the installation does not match approved documents, the exception should be recorded rather than informally accepted. Field teams should avoid assuming that a physically installed valve is automatically ready for energization or stroking.
How should piping cleanliness and mechanical readiness be reviewed?
The team should confirm that construction debris, temporary blinds, flushing residues, loose fasteners, and installation supports have been addressed under the plant’s approved commissioning plan.
This article does not define site-specific safety steps such as isolation, depressurization, or permit requirements. Those must come from the project and plant procedures. From a valve handover viewpoint, the question is whether the valve is mechanically ready for controlled movement. Piping strain, flange alignment, gasket condition, accessible bolting, actuator bracket integrity, coupling security, and visible damage should be checked by the responsible discipline. If the valve was installed before line flushing or cleaning, the team should verify whether the commissioning procedure permits stroking and whether any protection remains in place.
What utility and wiring checks should be completed?
Utilities and wiring should be checked before functional commands are issued, because a valve may fail to move correctly if power, air, hydraulic supply, grounding, or signal wiring is incomplete.
For a pneumatic actuator, the team may need to confirm instrument air availability, pressure range required by the approved documents, tubing connections, regulator setup, exhaust path, and solenoid supply. For an electric actuator, supply voltage, cable termination, grounding, enclosure condition, and local control power should be checked according to project documents. For any actuated valve, signal wiring should be verified between the field device and the control system. Commissioning should avoid undocumented temporary jumpers or forced signals unless specifically authorized and recorded by the site procedure.
How should command, feedback, and travel be verified?
The team should prove that each command produces the intended valve movement and that feedback signals accurately represent the actual valve position.
This includes checking open command, close command, stop or hold functions where applicable, position feedback, open and closed limit indication, and any analog signal used for modulating service. The physical valve position should be observed, not inferred only from the control screen. Stroke direction must be confirmed because reversed action can create serious confusion during startup. Travel limits should be checked so the actuator does not overtravel, undertravel, or stop before the valve reaches its intended seat or travel position. For modulating valves, this check is separate from loop tuning and process performance testing.
How should local, remote, and interlock functions be handled?
Local and remote modes should be verified under approved procedures, and interlocks should be tested or confirmed according to the site commissioning plan.
The purpose is to ensure that control authority is clear. A valve may be operable from a local station, actuator selector switch, control room, safety system, or maintenance interface. Before handover, the team should know which mode is normal for operations and which modes are restricted. Interlocks should not be bypassed casually to “get the valve moving.” If an interlock prevents movement, that result may be correct. If a bypass or override is authorized for testing, the record should show the reason, approval, duration, and restoration status.
Which checks belong in a commissioning decision matrix?
A decision matrix helps the team separate readiness issues from defects, documentation gaps, and items that require formal acceptance.
Mechanical installation readiness
Primary question: Does the installed valve match the approved tag, location, flow direction, and orientation?
Typical evidence: Field inspection record, drawing reference, tag verification, installation punch item status.
Handover decision: Accept only if deviations are closed or formally listed as approved exceptions.
Utility readiness
Primary question: Are air, power, hydraulic supply, or other required utilities available and correctly connected?
Typical evidence: Utility checklist, cable or tubing verification, instrument air or power availability record.
Handover decision: Do not perform uncontrolled stroking if required utilities are incomplete or unstable.
Signal and feedback integrity
Primary question: Do commands, indications, and position feedback match actual valve movement?
Typical evidence: I/O check sheet, control-system display capture, field observation record.
Handover decision: Hold handover if command direction or feedback status is ambiguous.
Travel and limit verification
Primary question: Does the valve reach the intended open, closed, or modulating travel range without abnormal restriction?
Typical evidence: Stroke test record, limit switch setting record, observed travel notes.
Handover decision: Accept only after travel limits are verified under the approved procedure.
Interlocks and operating mode control
Primary question: Are local, remote, permissive, trip, and override functions understood and documented?
Typical evidence: Cause-and-effect reference, control narrative, interlock test record, bypass log where applicable.
Handover decision: Do not transfer unresolved bypasses or unexplained interlock defeats to operations.
Documented exceptions
Primary question: Are remaining issues visible, owned, risk-reviewed, and approved for handover?
Typical evidence: Punch list, exception register, responsible person, target closure date.
Handover decision: Operations should receive a controlled exception list, not informal verbal promises.
What are three common misconceptions about actuated valve commissioning?
Misconception: A successful factory test means field commissioning can be skipped. The more accurate view is that FAT and commissioning answer different questions. FAT may confirm supplier-side assembly or function, while commissioning confirms installed readiness with site utilities, wiring, controls, and procedures.
Misconception: If the valve moves, it is ready for operations. The more accurate view is that movement alone is not enough. Direction, travel, feedback, limits, mode control, and interlocks also matter.
Misconception: Interlock testing is only a control-system issue. The more accurate view is that valve response, actuator behavior, field wiring, and operating authority all influence whether an interlock works as intended.
How can teams apply the checklist during handover?
Use the checklist as a staged handover document, not as a loose reminder.
First, confirm the approved drawings, datasheets, I/O list, loop folder, control narrative, and commissioning procedure are available. Second, inspect the installed valve and actuator against the tag and installation documents. Third, verify utilities and wiring before issuing movement commands. Fourth, stroke the valve under controlled conditions and compare physical position with command and feedback. Fifth, confirm travel limits, local and remote modes, and interlocks according to the plant plan. Sixth, record all exceptions with owners and acceptance status.
Shanghai Juliang Valve Group is described in the supplied company information as a manufacturer focused on industrial valve products and intelligent fluid control systems. That context supports using actuated valve commissioning as an educational topic, but actual project acceptance should always rely on current project documents and site-approved procedures.
What practical example shows the difference between movement and readiness?
Consider a hypothetical pneumatic on-off valve installed on a utility line. During field checks, the actuator moves when air is applied. If the team stops there, the valve may appear ready. A fuller commissioning check might find that the control-room “open” indication appears when the valve is physically closed, or that the local selector was left in manual mode after testing.
The issue is not necessarily the valve hardware. It may be wiring, limit switch adjustment, actuator orientation, control-system mapping, or documentation mismatch. A disciplined actuated valve commissioning checklist forces the team to compare field reality with the operator’s expected view. That is the difference between a valve that merely moves and a valve that operations can understand and control.
How should documented exceptions be treated before operations accepts the valve?
Exceptions should be visible, specific, approved, and assigned before handover.
A vague note such as “minor issue to be fixed later” is not enough. The record should identify the tag, the issue, the affected function, the temporary operating limitation if any, the responsible owner, and the required closure action. If the valve is accepted with an open punch item, operations should understand what has not been completed. Safety-critical, regulatory, or process-critical exceptions should follow the project’s approval route. Commissioning teams should not convert unresolved technical uncertainty into an informal operational burden.
Frequently Asked Questions
What should an actuated valve commissioning checklist include?
An actuated valve commissioning checklist should include tag verification, installation orientation, piping readiness, utility supply, electrical and signal wiring, command response, position feedback, stroke direction, travel limits, local and remote modes, interlocks, and documented exceptions. The exact checklist should be aligned with the plant commissioning plan, approved drawings, control philosophy, and applicable site safety requirements.
Is valve commissioning the same as a factory acceptance test?
No. A factory acceptance test is normally performed before shipment or release and may confirm agreed supplier-side checks. Commissioning is performed after installation and verifies the installed valve within the actual field environment. It considers site wiring, utilities, control logic, interlocks, operator interfaces, and the current condition of the piping system.
Should a commissioning team stroke every actuated valve before handover?
Stroking is commonly part of commissioning, but it should only be done when allowed by the approved site procedure. The team must consider process conditions, isolation status, mechanical readiness, utilities, and interlocks. Some valves may require staged testing, restricted movement, or special authorization depending on service, system status, and plant rules.
Who should accept an actuated valve for operations?
Acceptance usually involves commissioning, instrumentation, mechanical, control-system, and operations representatives, depending on the project organization. The important point is that acceptance should be documented. Operations should receive clear evidence of completed checks, any approved exceptions, and the normal control mode expected after handover.
What happens if command and feedback do not match during commissioning?
If command and feedback do not match, the valve should not be treated as ready until the cause is understood. Possible causes include reversed wiring, incorrect limit switch settings, actuator orientation issues, control-system mapping errors, or mechanical travel problems. The discrepancy should be recorded, investigated, corrected, and retested under the approved commissioning procedure.
Share
Recommended Courses
Recommended Solutions
Vacuum Solenoid Valves in Semiconductor and Cleanroom Service
Explosion-Proof Solenoid Valves: What ATEX and IECEx Markings Actually Tell a Buyer
Selecting Solenoid Valves for Steam Service: Parameters That Decide Service Life