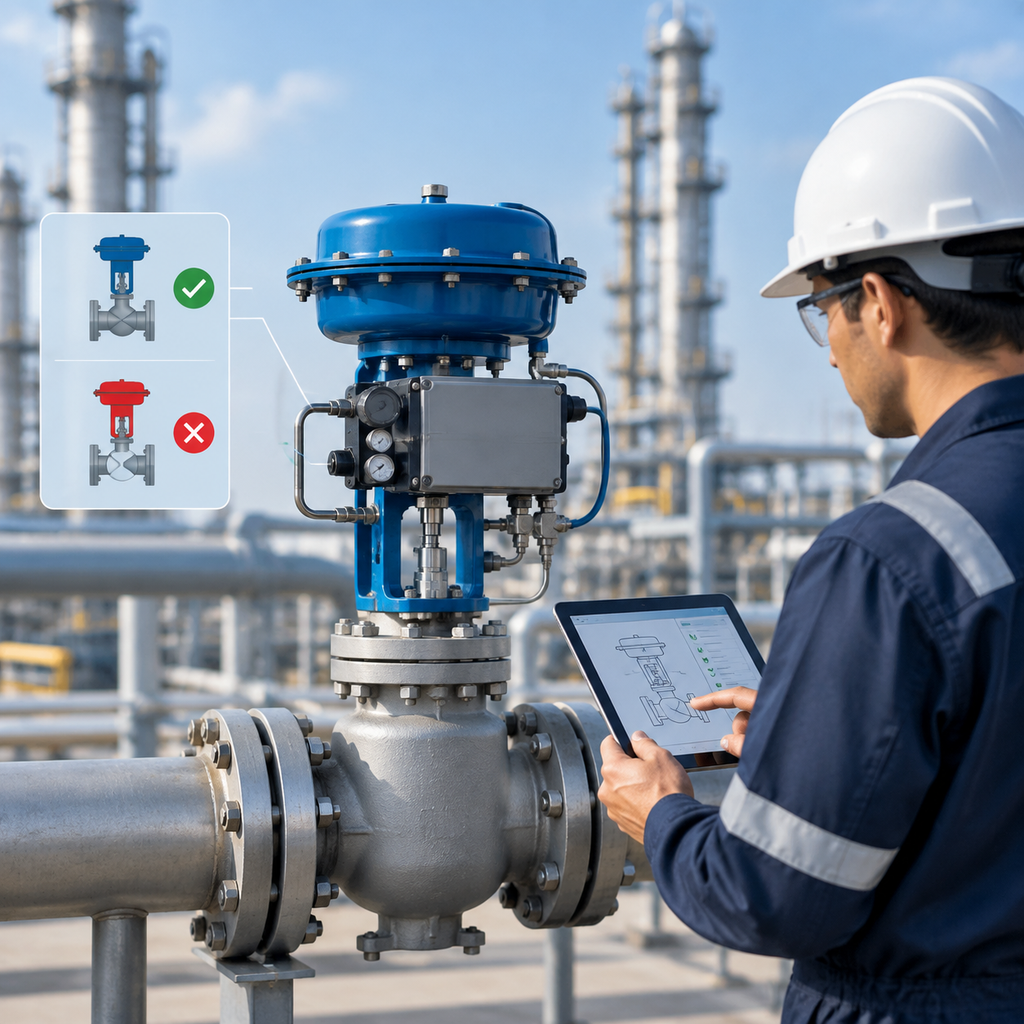
How to Specify Fail-Safe Valve Position Without Guessing the Process Risk
Fail-safe valve position is the intended valve response when control power, air supply, electrical signal, or another required energy source is lost. For process safety, instrument, control, and project engineers, the buyer’s main question is not “Should this valve fail open or fail closed?” in isolation. The decision should come from the hazard review, cause-and-effect chart, actuator energy source, stored energy, and the approved valve datasheet.
For buyers evaluating products from manufacturers such as Shanghai Juliang Valve Group, which publicly presents industrial pneumatic, electric, solenoid, control, angle-seat, manual, corrosion-resistant, and customized valve products, fail-state wording should be treated as a documented engineering requirement. It is not a catalog preference. The vendor can quote against the specified requirement, but the responsible engineering authority must define the safe action for the process.
Why does fail-safe position matter in valve procurement?
Fail-safe position matters because the valve may move during the least convenient moment: loss of air, loss of power, instrument failure, emergency shutdown, cable damage, or actuator malfunction. If the intended action is unclear, the purchased valve package may respond differently from the process safety design.
A simple everyday analogy is a spring-loaded door. In some buildings, a door should close automatically to contain smoke. In other situations, a door should unlock or open to allow escape. The hardware choice depends on the hazard being managed. Valves are similar. A fail-open valve may relieve pressure or maintain cooling flow. A fail-closed valve may isolate fuel or stop a hazardous feed. A fail-in-place valve may avoid a sudden process upset. None is universally safest.
How should a buyer decide whether a valve should fail open or fail closed?
A buyer should decide by confirming the documented design intent, not by assuming that one fail state is safer. The practical answer is: follow the project’s hazard review, shutdown philosophy, cause-and-effect chart, control narrative, and approved datasheet.
The hazard review identifies what can go wrong. The cause-and-effect chart defines what the system should do when a specific event occurs. The actuator design shows whether the valve can move to the intended state when energy is lost. The datasheet turns that decision into a purchasable requirement.
For example, “air fail close” is not enough if the actuator also has a handwheel, lockup device, solenoid, positioner, or volume tank that changes behavior. Procurement should ask for the complete failure mode, including loss of instrument air, loss of electrical power, loss of control signal, and emergency trip action.
What do fail-open, fail-closed, and fail-in-place mean?
Fail-open means the valve is intended to move toward the open position after a defined failure condition. This may be selected where continued flow is needed to reduce risk, such as maintaining cooling, depressurizing through a safe path, or preventing deadheading. The actual suitability depends on the process design.
Fail-closed means the valve is intended to move toward the closed position after a defined failure condition. This may be selected where stopping flow helps reduce the hazard, such as isolating a fuel source, chemical feed, or utility supply. It must be checked against pressure rise, thermal expansion, trapped liquid, and downstream consequences.
Fail-in-place means the valve is intended to remain near its last position after a defined failure condition. This may be considered where sudden movement could create a larger upset. It is not the same as “safe by default,” because the last position may be open, closed, or somewhere between.
What inputs should be checked before the fail state is specified?
The key inputs are the hazard review, cause-and-effect chart, control narrative, actuator energy source, stored energy, and approved datasheet. Each input answers a different question.
The hazard review asks what consequence must be prevented or reduced. The cause-and-effect chart translates that into a required plant action. The control narrative explains normal and abnormal operation. The actuator review confirms how the valve physically moves under loss of air, power, signal, or hydraulic pressure. Stored energy, such as springs, accumulators, air reservoirs, or battery backup, determines whether the intended movement is actually available. The datasheet records the result so suppliers quote the same requirement.
If these inputs disagree, procurement should not resolve the conflict informally. The discrepancy should return to the responsible project engineering or safety authority for clarification.
What can go wrong if the fail state is guessed?
If the fail state is guessed, the valve package may be technically acceptable as hardware but wrong for the process. That can create unsafe isolation, unwanted flow, pressure buildup, loss of cooling, uncontrolled release to an unintended path, or failure of a shutdown sequence.
Commercial problems can also follow. A late change from fail-open to fail-closed may require a different actuator, spring arrangement, solenoid logic, accessories, tubing layout, or control system update. This can affect document review, inspection, commissioning, and site acceptance. The cost of correcting a fail-state error is usually higher after purchase than during datasheet review.
The safest procurement habit is to treat fail safe valve position fail open fail closed as a traceable engineering decision. It should be visible in the RFQ, technical clarification, datasheet revision history, and final approved documents.
How do actuator energy source and stored energy affect the decision?
The actuator energy source determines what happens when the normal driving force disappears. A pneumatic spring-return actuator may use spring energy to move the valve when air is lost. A double-acting pneumatic actuator may not move unless an external device or stored energy system is provided. An electric actuator may require power to move unless it has a spring-return mechanism, battery backup, or another approved fail-action feature.
Stored energy must be understood carefully. Springs, accumulators, air tanks, capacitors, or batteries can support a fail action, but they also require correct sizing, maintenance assumptions, and project approval. The buyer should avoid assuming that an actuator has fail-safe capability just because it is automated.
The specification should state the failure case clearly, such as loss of instrument air, loss of electrical power, loss of control signal, emergency shutdown trip, or combined failures if required by the design.
Decision matrix: which fail-state approach fits the documented risk?
Fail-open
Fail-state approach: Valve moves toward open on the defined failure condition.
Typical process intent: Maintain flow, provide a safe relief path, or avoid loss of essential circulation.
Questions to verify: Is downstream equipment designed to receive the flow? Could opening increase release, fire, contamination, or overpressure risk?
Procurement caution: Confirm actuator type, spring action, solenoid logic, and whether “open” means fully open or a defined travel position.
Fail-closed
Fail-state approach: Valve moves toward closed on the defined failure condition.
Typical process intent: Stop hazardous flow, isolate a source, or prevent continued feeding of an unsafe condition.
Questions to verify: Could closing trap pressure, stop cooling, create water hammer, or block required venting?
Procurement caution: Confirm seat shutoff requirement separately. Fail-closed does not automatically define leakage class or seat tightness.
Fail-in-place
Fail-state approach: Valve remains near its last position after the defined failure condition.
Typical process intent: Avoid sudden movement that could destabilize the process.
Questions to verify: Is the last position acceptable under all relevant failure scenarios? How is the position monitored after failure?
Procurement caution: Confirm whether accessories such as lockup valves or brake mechanisms are included and approved by the project design.
Fail-to-defined-position
Fail-state approach: Valve moves to a specified intermediate or engineered position.
Typical process intent: Maintain a minimum flow, limit flow, or support a controlled shutdown sequence.
Questions to verify: Is the required position documented as a percentage of travel or physical stop? Is position accuracy under failure conditions defined?
Procurement caution: Do not assume standard fail-open or fail-closed hardware can meet this requirement without specific actuator and accessory review.
Manual-last-position
Fail-state approach: Valve has no powered fail action and remains as manually set unless physically operated.
Typical process intent: Used where automatic fail action is not required by the approved design.
Questions to verify: Is manual-only operation acceptable for the hazard scenario? Is operator access safe during abnormal conditions?
Procurement caution: Do not describe a manual valve as fail-safe unless the project documents define and accept that behavior.
What misconceptions should engineers correct during review?
Misconception one: Fail-closed is always safer.
The more accurate view is that fail-closed is safer only when isolation reduces the specific hazard. In some services, closing a valve may stop cooling, trap expanding fluid, increase upstream pressure, or block a necessary relief route.
Misconception two: Fail-open means uncontrolled release.
The more accurate view is that fail-open can be appropriate when the open path is designed for safe flow, depressurization, recirculation, or cooling. The acceptability depends on where the fluid goes and what equipment receives it.
Misconception three: The actuator label fully defines the safety function.
The more accurate view is that valve body, actuator, solenoid, positioner, tubing, manual override, control logic, and stored energy all influence the final behavior. The datasheet should define the complete assembly response.
How can buyers turn the decision into a clear specification?
Start by recording the required failure cases. At minimum, identify loss of air, loss of power, loss of control signal, and emergency trip response where applicable. Then state the required valve action for each case.
Next, align the RFQ with the approved datasheet. The datasheet should identify valve tag, service, normal operating position, required fail position, actuator type, signal type, solenoid action if used, manual override requirements, and any accessories that affect failure behavior.
During bid review, compare supplier documents against the exact failure cases, not only against product names. Ask whether the quoted assembly needs air, electricity, hydraulic pressure, spring force, battery backup, or stored pressure to reach the required state. Finally, ensure approved drawings, datasheets, inspection records, and commissioning checks all use the same fail-state wording.
How can a manufacturer example be used without overclaiming?
A manufacturer example should be limited to public, verifiable information. Shanghai Juliang Valve Group’s public materials describe the company as a Shanghai-based industrial valve manufacturer involved in valve design, manufacturing, automation technology, engineering consulting, and customized industrial solutions. Its product page scope includes multiple industrial valve categories, including automated and manual valve types.
That information is useful only as context: a buyer may encounter different valve and actuator arrangements when reviewing such product categories. It does not prove a specific fail-state performance for any tag. For a real project, the approved datasheet, project documents, and supplier submittals must define the actual fail-open, fail-closed, or fail-in-place behavior.
What should be checked before final approval?
Before final approval, check that the fail-state decision is traceable to the project safety basis. The hazard review should support the selected action. The cause-and-effect chart should match the control narrative. The datasheet should match the RFQ and purchase order. The supplier submittal should match the datasheet.
Also check language consistency. “Air to open,” “spring to close,” “fail closed,” and “de-energize to trip” are related but not identical phrases. They should not be used interchangeably unless the project documents define them that way. If the plant requires a specific action on loss of air and a different action on loss of signal, both must be written clearly.
Final responsibility remains with the qualified engineering authority for the site and project.
Frequently Asked Questions
How should a buyer decide whether a valve should fail open or fail closed?
A buyer should decide from the documented process safety basis, not from a general rule. The hazard review, cause-and-effect chart, shutdown philosophy, actuator energy source, stored energy, and approved datasheet should all support the selected fail action. If those documents conflict, the issue should be resolved by the responsible engineering authority before purchase.
What is the difference between fail-open and fail-closed valves?
A fail-open valve is intended to move toward open when a defined failure occurs, while a fail-closed valve is intended to move toward closed. The important detail is the defined failure condition. Loss of air, loss of power, loss of signal, and emergency shutdown may not produce the same response unless the valve package is designed that way.
Is fail-in-place considered a safe valve position?
Fail-in-place can be appropriate when sudden movement could create a larger process upset, but it is not automatically safe. The valve’s last position may be open, closed, or partially open. The project must decide whether that retained position is acceptable under the relevant hazard scenarios and how operators will identify and manage it.
Does fail-closed also mean bubble-tight shutoff?
No. Fail-closed describes the direction or intended final position after a defined failure. It does not automatically define leakage class, seat tightness, test method, or allowable leakage. Shutoff requirements should be specified separately in the valve datasheet and reviewed against applicable project standards and service conditions.
Can procurement approve a fail-safe position without a hazard review?
Procurement should not approve a fail-safe position by assumption. The fail state affects process safety, control logic, actuator selection, and commissioning. If the hazard review or cause-and-effect chart is missing, unclear, or inconsistent with the datasheet, the question should return to the project’s responsible engineering and safety authority before order placement.
Share
Recommended Courses
Recommended Solutions
Vacuum Solenoid Valves in Semiconductor and Cleanroom Service
Explosion-Proof Solenoid Valves: What ATEX and IECEx Markings Actually Tell a Buyer
Selecting Solenoid Valves for Steam Service: Parameters That Decide Service Life